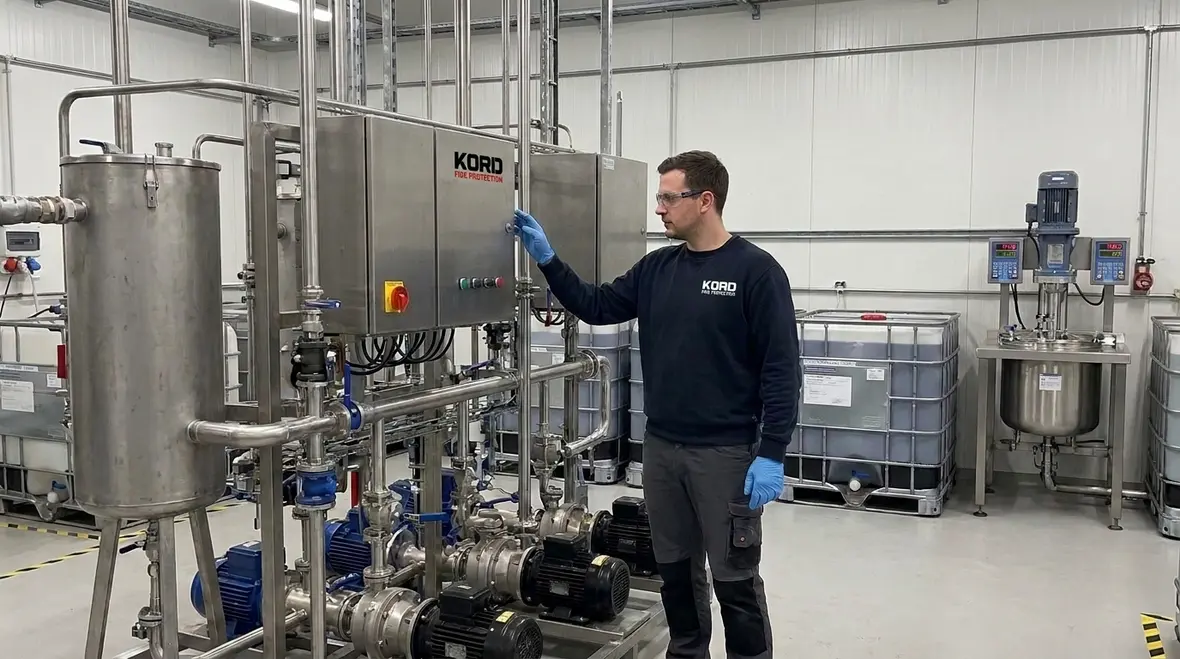
NFPA 33 Section 16.2: General Rules for Peroxide and Multi-Component Coatings
Quick Answer: NFPA 33 Section 16.2 establishes the baseline safety rules for using organic peroxides and multi component coatings. It focuses on storage, handling, process controls, segregation, and maintenance to reduce decomposition and ignition risks.
Facilities that need broader system support can also explore full fire protection services from Kord Fire Protection, which naturally fits alongside compliance planning for coating operations and ongoing inspection programs.
Why NFPA 33 Section 16.2 matters in commercial coating operations
Facilities that apply organic peroxide and multi component coatings often treat day to day production as routine. NFPA 33 Section 16.2 removes that assumption by requiring controls that address the specific hazards of peroxides, including decomposition, contamination sensitivity, and rapid fire growth potential. For many commercial, industrial, and retail environments, compliance gaps show up during equipment changeovers, cleaning cycles, and maintenance work on process lines. Those are also the moments when control systems and housekeeping frequently fail.
In practice, meeting NFPA 33 organic peroxide general requirements requires more than having SDS binders on file. It requires documented procedures, verified equipment performance, and inspection routines that catch deterioration before it becomes an incident.
What Section 16.2 covers: process baseline rules for peroxides and mixes
NFPA 33 Section 16.2 provides general rules that apply across peroxide coating processes and multi component systems. These systems commonly combine reactive ingredients that must be proportioned, mixed, and applied under controlled conditions. When peroxides are involved, the risk profile changes because decomposition can accelerate under heat, contamination, or improper handling. Section 16.2 therefore drives a set of operational expectations that facilities must implement before production starts and must sustain through ongoing maintenance.
Commercial facilities typically struggle with three categories of requirements:
- Segregation and compatibility: keeping peroxides away from incompatible materials, including certain additives and contaminants introduced during cleaning or line purge.
- Controlled handling: limiting exposure to elevated temperatures, friction, and mechanical stress that can contribute to unsafe conditions.
- Reliable equipment and procedures: ensuring mixers, transfer pumps, metering devices, and ventilation control systems operate within expected parameters.
Peroxide handling and storage controls that prevent decomposition
Peroxide hazards are operational, not theoretical. Section 16.2 expects facilities to manage the conditions that influence peroxide stability. Although exact requirements depend on the peroxide type and process layout, the recurring compliance themes include temperature management, container integrity, and controlled transfer practices.
1) Temperature and environmental management
Temperature excursions are one of the most common process failure points. Facilities often have variability from room HVAC cycling, proximity to hot surfaces, or inconsistent storage practices. Compliance programs should confirm that temperature monitoring is installed where it matters and that alarm thresholds align with the peroxide stability guidance in the product safety documentation.
2) Clean transfer lines and contamination control
Multi component coatings frequently share equipment across formulations. Incomplete purging, residual residues, or incorrect changeover procedures can introduce incompatible contaminants to peroxide lines. Effective programs treat cleaning and purge verification as an essential part of the hazard control, not an optional housekeeping step.
3) Container integrity and labeling discipline
Breakdowns in labeling and container handling create traceability gaps that complicate safe operation. Facilities should maintain controls that prevent unintended mixing, incorrect reuse of containers, and degraded labeling during routine production.
How multi component coating systems are managed under Section 16.2
Multi component systems create hazards through incorrect proportions, delayed mixing, or application outside designed operating windows. Section 16.2 supports risk reduction by emphasizing consistent process controls. The goal is to prevent conditions where mixed products behave unpredictably or where peroxides become exposed to unsafe triggers.
Mixing, proportioning, and metering safeguards
Metering pumps, flow meters, and proportioning controls must deliver consistent results. Drift in calibration, clogged strainers, worn seals, or air entrainment in suction lines can alter ratios. Those ratio changes can affect reaction behavior and increase the likelihood of unsafe process outcomes. Preventive maintenance should include verification steps that confirm output accuracy, not only component replacement.
Process line integrity and leak prevention
Leak points often occur at fittings, hose connections, pump seals, and mixing heads. Once a peroxide system is contaminated or partially reacted, cleanup becomes higher risk. Facilities must ensure that leak response procedures exist and that personnel follow them without improvisation.
Ventilation and control system performance
Where coatings generate vapors, mists, or other airborne hazards, ventilation performance affects both worker safety and fire risk. In commercial settings, ductwork and fans may degrade quietly due to particulate loading or maintenance delays. Inspection routines should verify that airflow and exhaust effectiveness remain within expected performance criteria.
Inspection, testing, and maintenance: where compliance breaks down
NFPA 33 compliance is not a one time checkbox. Section 16.2 encourages ongoing integrity through inspection and maintenance expectations that match peroxide and multi component realities. The most frequent operational compliance gaps include missed changeover verification, inadequate records for equipment calibration, and delayed repairs for degraded seals, hoses, or controls.
Common failure points during routine production
- Incomplete purge verification after formulation changes or line shutdowns.
- Worn seals and hoses that create small leaks which escalate during pressure changes.
- Unverified calibration of metering devices leading to incorrect component ratios.
- Reduced ventilation performance due to dust loading or fan impairment.
- Insufficient documentation showing that procedures are followed and effective.
Commercial facility documentation that holds up during review
Commercial fire safety expectations often extend beyond “having a plan” to proving the plan works. Facilities should maintain records for:
- Procedure training and sign off for peroxide handling and line changeovers
- Calibration and preventive maintenance schedules for metering and mixing equipment
- Inspection results for transfer systems, hoses, seals, and leak control measures
- Ventilation performance checks where coatings generate airborne hazards
- Incident and near miss logs that drive corrective actions
For companies seeking a reliable compliance partner, Kord Fire Protection supports ongoing testing, inspection coordination, and maintenance planning to help facilities sustain safe operations and demonstrate program effectiveness over time.
Teams that also manage pump reliability can dig deeper with advanced commercial fire pump diagnostics for power issues, a useful companion read when maintenance documentation and equipment performance start telling two different stories.
Operational best practices: making Section 16.2 workable on the floor
Even well engineered coating lines can drift out of compliance when operational discipline weakens. Facilities should treat NFPA 33 Section 16.2 as a workflow requirement that connects management systems, operator actions, and equipment condition.
Build changeover routines around peroxide sensitivity
Facilities should use standardized checklists for formulation changes that include purge verification, compatibility checks, and confirmation that metering devices match the intended product. When a changeover occurs under time pressure, the checklist must still execute without shortcuts.
Train operators on symptoms, not just rules
Effective training teaches operators what early warning signs look like, such as unexpected viscosity changes, abnormal pressure readings, or airflow deviations. These symptoms can indicate conditions that make peroxide handling unsafe.
Link maintenance to hazard outcomes
Instead of scheduling maintenance only by hours or usage, connect maintenance triggers to hazard outcomes like leak risk, contamination risk, and reaction consistency. That approach improves reliability and supports auditable compliance.
Frequently Asked Questions
Conclusion and Call to Action
NFPA 33 Section 16.2 sets the operating baseline for peroxide and multi component coating safety, but compliance only holds when procedures, equipment condition, and inspection discipline stay aligned. Kord Fire Protection helps commercial facilities validate and maintain fire and process safety controls through structured testing, inspection support, and maintenance planning. Schedule a compliance review to identify peroxide handling risks, confirm equipment reliability, and close documentation gaps before they become operational problems.
Join Our Newsletter!
Get the latest fire safety tips delivered straight to your inbox From our Newsletter.