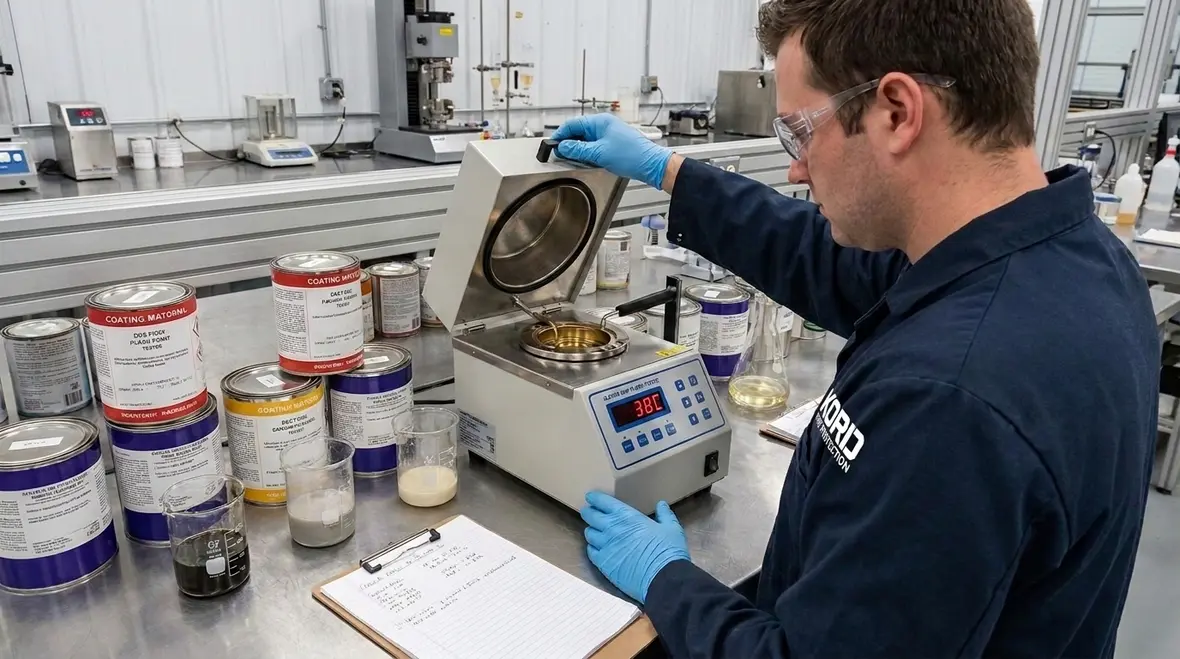
NFPA 33 Section 4.8: Determining Flash Point of Mixed Coating Materials
Quick Answer
NFPA 33 Section 4.8 requires a defensible method to determine the flash point of mixed coating materials. Commercial operators must use documented testing and reliable calculations, then verify results against storage and process classification requirements to maintain safe, code-compliant handling.
For teams tightening documentation and audit readiness around coating hazards, Kord Fire Protection’s fire safety system documentation for compliance resource is a practical place to start before the binder starts acting like a mystery novel with missing pages.
Why mixed coatings create flash point risk under NFPA 33
Mixed coating systems commonly combine multiple solvents, reactive diluents, and specialty additives. Each component can contribute different volatility and ignition characteristics. As a result, a single component flash point does not automatically represent the fire hazard of the finished blend. This is where NFPA 33 flash point determination mixed coatings becomes critical for accurate classification, permitting, ventilation design basis, and safe operating controls in commercial facilities such as industrial coating lines, finishing rooms, and retail distribution environments.
Operationally, facilities often face compliance friction when formulation changes occur without an updated hazard evaluation. Even small variations in supplier lots, temperature, viscosity targets, or blending ratios can shift the effective flash point enough to move materials into a different storage or handling category.
What Section 4.8 expects: a documented flash point basis
NFPA 33 Section 4.8 focuses on determining flash point for mixtures in a way that supports safe classification and control. The main compliance expectation is traceability. Facilities should be able to show that the flash point value used for risk controls reflects the actual mixture intended for use, and that the method used to obtain or calculate it is documented, repeatable, and consistent with recognized test practice.
Common compliance elements auditors look for
- Mixture identity: formulation sheet showing the exact components and blending ratio used for the tested or evaluated mixture.
- Testing or approved basis: evidence that the flash point came from testing of the mixed material, or from an approved approach supported by the code intent and safety engineering rationale.
- Temperature and condition controls: documentation that sample preparation and test conditions were controlled and consistent with the method used.
- Version control: change management records showing when the hazard basis is updated due to formulation or supplier changes.
- Material use alignment: confirmation that the hazard basis matches the material actually sprayed, coated, thinned, or cleaned in the facility.
How facilities typically determine flash point for mixed coatings
In practical facility operations, flash point determination methods generally fall into two buckets: direct testing of the mixed coating and defensible calculation or selection based on component data. NFPA 33 Section 4.8 requires that the resulting flash point value used for classification is not a guess. It must reflect the blend in a way the facility can support during inspections, insurance reviews, and internal safety audits.
Direct testing of the mixed coating blend
Direct testing tends to reduce uncertainty because the test measures the behavior of the finished mixture. Facilities typically prepare a representative batch using the intended ratio of solvents and additives, then test using an accepted flash point procedure. This approach is especially important when components are chemically reactive, when surfactants or co-solvents alter evaporation profiles, or when proprietary blends limit the usefulness of component level data.
Operational best practices for testing readiness:
- Use the same container type and transfer method the production system uses, since headspace and transfer losses can change composition.
- Control ambient temperature during sampling and handling, since volatility can drift quickly in coating operations.
- Retain batch records and sample traceability so the tested mixture can be matched to the material used in the field.
- Plan for retesting when formulation changes, even if the label remains similar, because functional performance targets often drive ratio shifts.
Calculation or selection based on component flash point data
Where a facility uses a calculation approach, it still must show that the method and inputs produce a defensible mixture flash point. The biggest failure points include relying on outdated Safety Data Sheets, using component flash points that do not match actual supplier lots, or treating blending as a simple averaging problem. For mixed coating systems, the volatility and vapor space effects can make simplistic approaches misleading.
Common failure points:
- Component data not updated after supplier changes.
- Assuming temperature-independent behavior, despite real operational heating and batch aging.
- Ignoring diluent additions performed on-site, such as thinners, reducers, or cleaning solvents.
- Using an inferred mixture flash point when the actual process uses a different ratio or batch conditioning.
Facility compliance impact: classification, storage, and ignition control
Once a credible flash point for the mixed coating material is established, it drives multiple compliance decisions. In commercial facilities, the flash point basis affects how the material is classified for storage capacity limits, container and transfer safety requirements, and the design and operation of ignition control systems.
Where flash point values affect day to day operations
- Storage room and cabinet requirements: the flash point basis can change what quantities are allowed and what separation or enclosure controls apply.
- Ventilation design basis: flash point influences the control strategy for vapor accumulation, especially during mixing, spray, and cleaning.
- Hot work and ignition source control: operations often align work permits, electrical equipment selection, and housekeeping zones with flammability expectations derived from the hazard basis.
- Labeling and SDS cross checks: hazard communication should align with the determined flash point basis used for safety controls.
In many commercial and industrial settings, coating workflows change faster than the compliance documentation cycle. Facilities that maintain a formal hazard basis review process reduce the chance of mismatches between current production chemistry and the controls written in the compliance binder.
Inspection readiness: evidence packages and maintenance controls
Successful compliance under NFPA 33 typically depends on having an auditable evidence package. Fire safety professionals should expect inspections to focus not only on the flash point number, but on the method and maintenance discipline behind it.
Build a defensible evidence package
- Flash point determination report: method used, sample preparation details, and test or calculation documentation.
- Formulation sheet: component list, blending ratio, and any on-site additions.
- Change control log: records of formulation changes, supplier lot updates, and any revalidation actions.
- Training and SOP alignment: spray, mixing, and cleaning procedures that match the hazard controls tied to the flash point basis.
- Inventory and transfer records: evidence that the material stored and used aligns with the evaluated mixture composition.
Ongoing maintenance requirements that prevent drift
Flash point determination is not a one time paperwork task. Facilities should schedule rechecks when any of the following occur: formulation changes, additive substitutions, new supplier approvals, changes in on-site thinning practices, or notable changes in process temperature or curing time that affect solvent behavior.
For commercial facilities that want to reduce compliance rework, Kord Fire Protection supports ongoing NFPA and fire code readiness through inspection support, documentation review, and maintenance planning aligned to real operational workflows. This helps teams keep hazard classifications synchronized with actual production chemistry.
To strengthen your overall compliance program, facilities can also review related guidance on fire safety compliance management with automated documentation and fire protection compliance auditing through Kord Fire Protection’s service resources.
Frequently Asked Questions
Conclusion and call to action
NFPA 33 flash point determination mixed coatings requires more than a number. Facilities need a documented, traceable basis aligned to the actual blend used, plus maintenance controls that prevent hazard classification drift. Kord Fire Protection can help your team compile an inspection-ready evidence package and keep flash point and related fire safety controls synchronized with ongoing operations. Contact Kord Fire Protection to schedule a compliance review and maintenance planning support.
Join Our Newsletter!
Get the latest fire safety tips delivered straight to your inbox From our Newsletter.