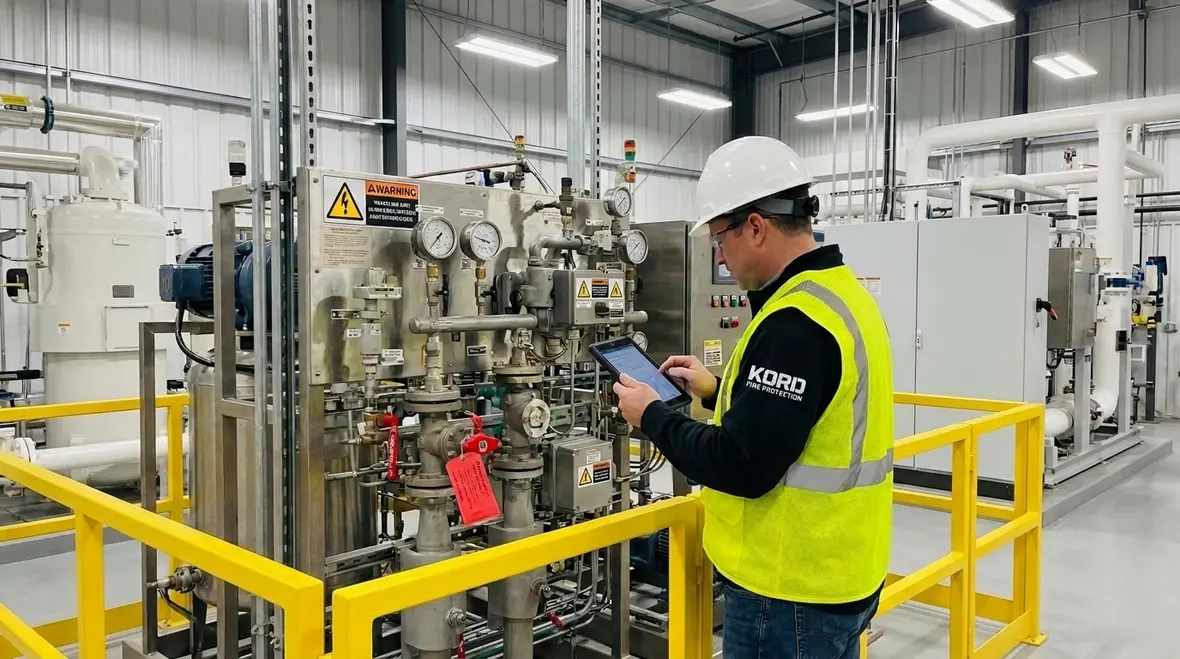
NFPA 32 Section 9.3 Processes and Equipment for Type IV Facilities
Quick Answer: NFPA 32 Section 9.3 sets minimum compliance expectations for how Type IV facilities manage and maintain process equipment. These requirements focus on design integrity, safe operation, installation details, and inspection or impairment prevention so systems remain reliable under normal and abnormal conditions.
Facilities working through industrial hazard controls often benefit from a broader commercial fire suppression systems and services strategy, especially when process equipment risks overlap with suppression design, inspection, and long term maintenance planning.
Why NFPA 32 Section 9.3 matters in Type IV occupancies
Type IV facilities handle combustible dust, flammable liquids, or other hazards where process equipment can become an ignition source if it fails, leaks, overheats, or loses containment. This is why the NFPA 32 Type IV process equipment requirements are not limited to initial installation. Section 9.3 drives ongoing performance through inspection readiness, impairment control, and maintenance practices that sustain the designed safety functions.
From a practical compliance standpoint, commercial and industrial owners often encounter recurring gaps in documentation, missing maintenance records, and equipment modifications that were never evaluated for fire safety impact. A fire protection program must treat process equipment as part of a living safety system, not a one-time capex purchase.
What Section 9.3 expects for Type IV process equipment
NFPA 32 Section 9.3 addresses the processes and equipment used to produce, store, convey, and handle flammable and combustible materials in Type IV facilities. While exact details vary by process type, the core intent remains consistent: equipment must be installed correctly, operate within safe parameters, and remain free from conditions that significantly increase ignition probability.
Design and installation integrity
Process equipment should be compatible with expected chemical and thermal conditions. Compliance expectations typically include maintaining safe clearances, ensuring correct mounting and support, and using components rated for the operating environment. Key failure patterns include:
- Improper gasket selection or degraded seals that introduce vapor or dust leakage.
- Inadequate bonding and grounding, which can allow static accumulation near transfer points.
- Unapproved piping or duct modifications that disrupt flow patterns and containment.
- Use of wrong-rated electrical components near classified areas.
If hazardous area electrical details are part of the risk picture, Kord Electric’s guide to NEC hazardous location bonding adds useful context for facilities trying to reduce unsafe electrical conditions around classified spaces.
Safe operating conditions and controls
In many Type IV environments, safe operation depends on controls such as temperature limits, pressure monitoring, interlocks, and venting arrangements. Section 9.3 effectively requires owners to treat these controls as safety critical. Operational drift happens when setpoints change, sensors are bypassed, or alarms are disabled to avoid nuisance trips.
A common compliance challenge is that maintenance departments focus on mechanical reliability, while fire protection risk controls depend on electrical function, setpoint accuracy, and consistent response times. Both must be managed together.
Impairment prevention and maintenance discipline
NFPA 32 expectations align with a discipline model: equipment cannot be allowed to operate while impaired. Impairment often appears as:
- Broken or missing access panels that compromise inspection and maintenance.
- Dust collection system component damage that reduces capture efficiency.
- Belts, seals, and bearings failing in transfer equipment, increasing heat and friction.
- Vent or relief pathways partially obstructed by product buildup.
To manage these risks, facilities need a defined inspection cadence, documented corrective actions, and verification that repairs restore the equipment to its intended safety function.
Inspection, testing, and documentation that withstand audits
Section 9.3 is often interpreted as a maintenance and verification requirement as much as a design requirement. During audits, the most effective facilities can show that process equipment safety features remain functional over time.
Inspection focus areas for process equipment
Inspectors and AHJs typically expect evidence that the facility checks for issues that increase likelihood of ignition or reduce containment. Typical focus areas include:
- Leak detection and containment verification at transfer points and joints.
- Condition assessment for enclosures, doors, seals, and gasketing on processing equipment.
- Evidence that dust control and venting systems remain unobstructed and correctly operating.
- Verification that any hot surfaces remain within safe temperature limits.
- Electrical verification for any equipment that interfaces with classified locations.
Common failure points that show up during field checks
Field experience shows recurring issues that lead to impairment findings:
- Temporary repairs that became permanent, such as improvised clamps or non-rated replacement parts.
- Worn couplings, misalignment, and bearing degradation that increase frictional heat.
- Dust accumulation on or around equipment that was not addressed by a coordinated housekeeping and engineering plan.
- Inconsistent calibration of measurement devices used to control process parameters.
To reduce repeat findings, compliance programs should link inspection results to a corrective action workflow with ownership, due dates, and confirmation testing.
Teams tightening documentation practices may also want to review this related article on inspection, testing, and documentation discipline, since the same audit pain points tend to show up whenever safety systems are maintained loosely and recorded even looser.
Operational procedures: keeping process equipment within safe boundaries
Even when equipment meets design intent, operational practices can undermine compliance. Section 9.3 effectively requires that processes and equipment operate in a way that prevents dangerous conditions from developing unnoticed.
Start up, shutdown, and abnormal condition controls
Facilities should define procedures for normal start up and shutdown that include verification steps for safety critical components. For abnormal conditions, procedures should specify what triggers a safe shutdown, which alarms require immediate response, and how the facility prevents restart until unsafe conditions are corrected.
Operational risk often increases during:
- Product changeovers when seals and fittings may be reworked.
- Maintenance windows when guards and covers are removed and not fully restored.
- Temporary bypasses to keep production running.
Housekeeping and material management coordination
Type IV hazards are frequently affected by dust and residue accumulation. Equipment compliance depends on coordinated housekeeping, maintenance access, and material management. Housekeeping procedures should integrate with inspection plans so cleanup is not reactive only after incidents or visible buildup.
Where applicable, facilities should align housekeeping schedules with equipment run hours and seasonal operating conditions, because accumulation rates can shift based on humidity, ventilation, and process throughput.
Commercial compliance support: how Kord Fire Protection helps
Meeting NFPA 32 Section 9.3 expectations requires more than a binder. Kord Fire Protection supports commercial and industrial owners by helping translate code intent into practical inspection plans, documentation workflows, and maintenance verification that aligns with audit expectations.
For a broader look at ongoing support, explore fire protection services in Southern California to see how inspection, repair, emergency response, and compliance-focused service can be structured for consistent testing, monitoring, and improvement.
Facilities with more complex production hazards may also find useful context in industrial fire suppression system design and manufacturing fire suppression planning, especially when process equipment risk, suppression coverage, and documentation all need to behave like one coordinated plan instead of three separate headaches.
Kord Fire Protection also helps teams identify common impairment patterns in process equipment and coordinate corrective actions so the facility can maintain safe operating states between formal inspection cycles.
Frequently Asked Questions
Next steps for compliance readiness
Conduct a gap review of process equipment against NFPA 32 Section 9.3 expectations, then verify inspection intervals, impairment controls, and documentation completeness for Type IV areas. If your facility has frequent maintenance changes or production variability, prioritize a coordinated inspection and correction workflow. Engage Kord Fire Protection to help structure ongoing testing, maintenance verification, and audit-ready records so your NFPA 32 Type IV process equipment requirements remain met throughout the year.
Join Our Newsletter!
Get the latest fire safety tips delivered straight to your inbox From our Newsletter.