NFPA 15 Section 7.2 Extinguishment Densities: The 0.15-0.50 gpm/ft² Range Explained
Quick Answer
NFPA 15 Section 7.2 defines a design density range of 0.15 to 0.50 gpm/ft² for certain water spray extinguishment applications. This range reflects differences in fire load, sprinkler or nozzle performance, and obstruction effects. Correct application selection and hydraulic verification drive compliance.
If you want broader context before getting too cozy with the density math, Kord Fire’s NFPA 15 water spray fixed systems overview is a natural place to start, especially for sites trying to line up hazard scope, system intent, and real-world compliance planning. ([kordfire.com](https://kordfire.com/nfpa-15-section-1-1-water-spray-fixed-systems-in-australia/?utm_source=openai))
Why Section 7.2 Extinguishment Density Range Matters for Cable Trays and Conveyors
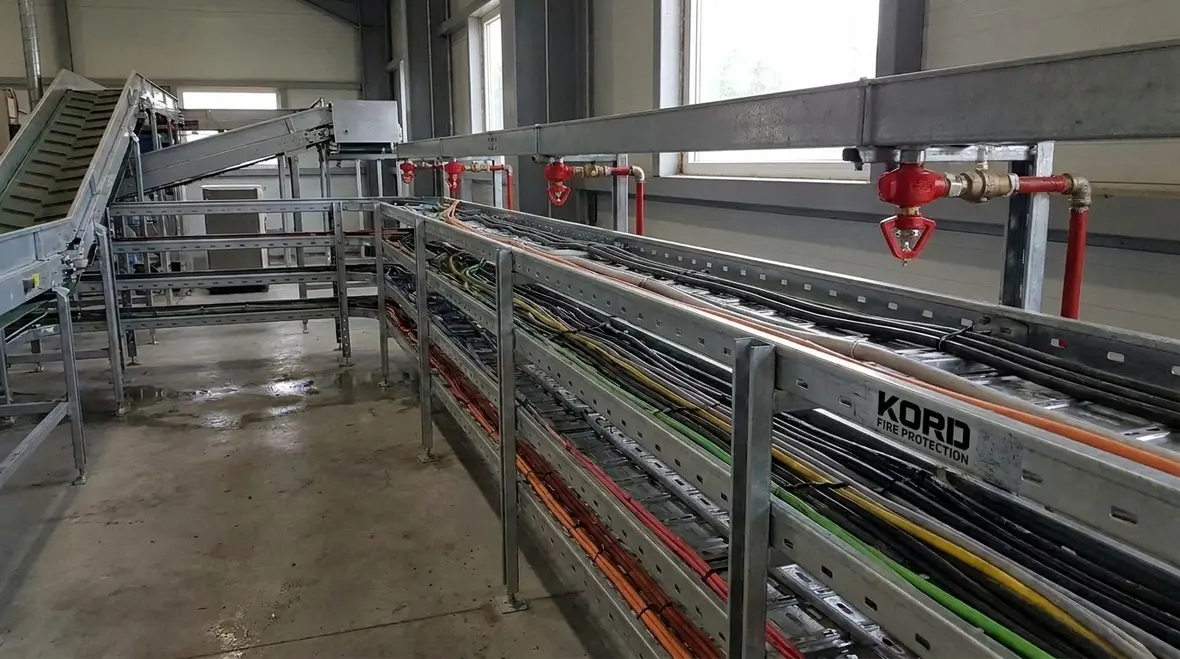
In facilities with cable trays and conveyor systems, the fire behavior is strongly influenced by how fire spreads along obstructions and the rate at which heat release increases as materials ignite. The NFPA 15 7.2 extinguishment design density 0.15 0.50 gpm/ft2 cable trays conveyors value selection is not arbitrary. It ties directly to the design assumptions used to size the water spray system and to confirm the system can deliver water where it must perform.
A common compliance challenge occurs when project teams apply a density that matches one room or one hazard category but fail to account for the specific obstruction geometry, coverage pattern, and expected fuel characteristics of cable trays, conveyor structures, and nearby combustible surfaces.
What NFPA 15 Section 7.2 Is Trying to Control
Section 7.2 extinguishment density is meant to ensure the system provides enough water application rate, over the design area and operating duration assumptions, to suppress and extinguish the specific hazard scenario. In practice, designers and inspectors use the density requirement as the anchor point for the entire hydraulic design package.
For commercial and industrial facilities, the densitiy range also reflects operational realities: water distribution can degrade due to nozzle spacing, elevation changes, piping limitations, and partial obstructions. The purpose of a higher density within the allowable band is to offset identified loss factors so the system still achieves the target performance.
How the 0.15 to 0.50 gpm/ft² range is typically used
The density you select within the permitted band should reflect the hazard severity and the expected difficulty of reaching and wetting burning surfaces. For cable trays and conveyors, this commonly depends on:
- Spacing and geometry of cable tray runs, cross supports, and covers that create shadowing effects.
- Presence of splices, bundle groupings, and cable jacket types that can increase ignition likelihood and flame spread.
- Conveyor construction and whether combustible materials are exposed, partially enclosed, or loaded intermittently.
- Whether the design area includes both direct exposure zones and adjacent surfaces likely to contribute to fire growth.
How Designers Translate Density Into System Hardware and Layout
NFPA 15 density requirements are only meaningful when the system design can actually deliver that application rate at the right locations. The design density determines the water demand, which then impacts pump sizing, pipe diameters, nozzle selection, and flow distribution across zones.
For readers looking at the water side of that equation, Fire Pumps has a practical guide on fire pump water supply considerations that fits naturally into design and verification discussions around demand, pressure, and system readiness. ([firepumps.org](https://firepumps.org/blog/bs-en-12845-water-supply-for-fire-pumps-guide/?utm_source=openai))
Hydraulic design checkpoints that often cause field issues
When density selection is correct on paper but performance fails in the field, the root cause is usually one of these:
- Inaccurate coverage assumptions: Cable trays and conveyor frames create obstruction patterns that can limit water penetration into the effective wetting area.
- Nozzle mismatch or incorrect spacing: A nozzle with a flow rate or spray pattern that does not match the design intent can reduce water distribution where it matters.
- Elevation and discharge angle problems: Spray deflection can increase when nozzles are placed to clear structures, changing where water lands.
- Pressure loss errors: Long pipe runs, fittings, and valves can drive actual nozzle pressure below design pressure, resulting in lower flow than intended.
- Zone boundary assumptions: If the design area selection is inconsistent with how equipment is actually arranged and loaded, the effective density can drop below the required level.
Obstruction and wetting performance for cable trays conveyors
Cable trays and conveyor structures typically create the conditions that require the sprinkler or nozzle arrangement to be resilient to “shadowing” effects. That is why the density range exists. Applying a value near the low end without verifying distribution effectiveness can lead to partial wetting, delayed suppression, and extended heating of exposed components.
In ongoing maintenance environments, additional real world variability appears. Cable additions, modifications to tray pathways, conveyor belt replacements, and housekeeping changes can alter the hazard geometry over time. A density that passed acceptance during construction can drift away from effective coverage if the layout changes without a corresponding engineering review.
Compliance and Maintenance: Where NFPA 15 Verification Usually Breaks Down
Many systems meet installation targets, but later inspection and operational performance reveals gaps. For owners, insurers, and facility managers, these are the recurring compliance pressure points tied to extinguishment density performance.
Inspection, testing, and performance verification
Maintenance and inspection activities must support the same assumptions used to set the NFPA 15 7.2 extinguishment design density 0.15 0.50 gpm/ft2 cable trays conveyors selection. This includes verifying:
- Nozzle condition and cleanliness, especially in environments with dust accumulation around cable trays and conveyor structures.
- Free and unobstructed discharge paths, including temporary storage areas that can develop after commissioning.
- System pressure within design limits during testing, with attention to valves, strainers, and sectional isolation devices.
- Proper setpoints and actuation performance for control components that maintain the correct flow demand at the design density.
Common failure points in commercial and industrial settings
Field failures rarely come from one dramatic event. They usually arise from a combination of smaller issues:
- Partially clogged nozzles: This reduces discharge and can silently reduce effective density across the design area.
- Unauthorized modifications: Adding cable bundles, moving tray segments, or altering conveyor enclosures can change wetting effectiveness without changing the hydraulics.
- Damaged piping support and alignment: Misalignment can cause spray distribution changes or create pressure loss variability.
- Seasonal operation and corrosion: Corrosion and scaling can reduce flow and elevate pressure losses over time.
Kord Fire Protection supports commercial compliance through commissioning support, periodic flow and pressure verification, and maintenance programs designed to keep the system performance consistent with the original NFPA 15 design intent. For additional background on fixed water spray system considerations and compliance planning, refer to NFPA 15 enhancing fire safety with water spray fixed systems.
If your team also needs more component-level context, Kord Fire’s article on NFPA 15 general system components requirements connects nicely with the maintenance and field-performance side of this discussion. ([kordfire.com](https://kordfire.com/nfpa-15-section-5-1-general-system-components-requirements/?utm_source=openai))
Planning for Ongoing Changes: Keep the Density Assumptions Current
Cable trays and conveyors are not static assets. Facilities reconfigure pathways, increase cable loading, expand production lines, and adjust conveyor routes. These changes can affect spray coverage, effective wetting, and the ability to achieve the selected density within the intended design area.
Practical owner and engineer workflow
To preserve compliance with extinguishment density targets, facilities should implement a workflow for change management:
- Trigger points: Treat additions to tray runs, new conveyor zones, major enclosure modifications, or any change that alters obstruction patterns as engineering review events.
- Document the as-built geometry: Maintain updated drawings that reflect tray spacing, conveyor structure, and the final nozzle layout.
- Confirm hydraulics where needed: If changes affect distribution, obstruction, or design area boundaries, confirm that system flow and pressure still deliver the required application density.
- Align testing schedules: Update maintenance and inspection checklists to include new or altered hazard zones.
Industry educational resources on fire pump and water supply considerations can support design and verification decisions. For general reference, see firepumps.org.
Frequently Asked Questions
Call to Action
If the facility has cable trays, conveyors, or recently completed modifications, Kord Fire Protection can help validate the system’s ability to deliver NFPA 15 extinguishment density performance through targeted inspection, testing, and maintenance planning. Schedule a compliance review to confirm distribution effectiveness, hydraulic readiness, and ongoing protection alignment before the next inspection cycle.
Join Our Newsletter!
Get the latest fire safety tips delivered straight to your inbox From our Newsletter.